Which service is right for you
Your starting point is the condition of the part and the level of protection required by the specification.
| Your condition | Applied | Output | Page |
|---|---|---|---|
| Serial profile and plate, repeated section | OMSG automatic turbine line | Sa 2½ or Sa 3, controlled surface profile | Steel Blasting |
| Heavy and different geometry manufacturing that does not fit in the automatic line | SAPI twin nozzle cabin, 26 m internal length | Same cleaning grades, without dividing the part | Large Part Blasting |
| Coated system to be applied on blasted surface | Airless wet painting, six resin families | Target DFT, layer-based record | Industrial Painting |
| Specification defines corrosivity category | Multi-layer system with ISO 12944 approach | Coating suitable for C3, C4 or C5 condition | ISO 12944 Corrosion Protection |
| Fire resistance period required on steel structure | Water or solvent-based intumescent system | DFT from R30 to R120 according to target | Fire Protective Coating |
Scope
Seven items performed in a single site. Subcontractor does not intervene from material acceptance to shipment coordination.
- 01 Surface preparation of steel structure, profiles, plates, and pipes
- 02 OMSG automatic turbine blasting and SAPI large part blasting
- 03 Wet paint systems based on epoxy, alkyd, zinc, aluminum pigmented, and polyurethane
- 04 Coating systems for C3, C4, and C5 corrosivity conditions on a project basis
- 05 Water and solvent-based intumescent and fire protective paint applications
- 06 DFT, climate, surface profile, and final quality controls
- 07 Packaging, storage, loading, and shipment coordination
Frequently asked questions
The most frequently asked questions during the quotation phase. If you cannot find what you are looking for, you can write directly.
You do not need to make a decision. Once the part information, current surface condition, and any existing specifications are provided, our technical team will determine the appropriate route, coating system, and scope of quality.
Yes. Surface preparation only or coating only requests can be accommodated. However, as the waiting time for a sandblasted surface is critical, performing both processes at the same facility offers an advantage in terms of quality.
Both are possible. Whether the supply is made by BER-GRİT or by the customer is clarified within the commercial scope. For customer supply, the product, batch, shelf life, and technical documents are recorded during incoming inspection.
Part list, weight and quantity, total surface area, desired Sa grade and profile, paint system or product code, number of coats, color, total DFT, desired quality tests, and target delivery date. Items you do not have can be left blank.
The turnaround time is calculated based on part dimensions, quantity, desired cleaning grade, number of coats, and curing time. Since the automatic line and booth are separate routes, serial jobs and project-based heavy parts do not delay each other.
Selections from applications
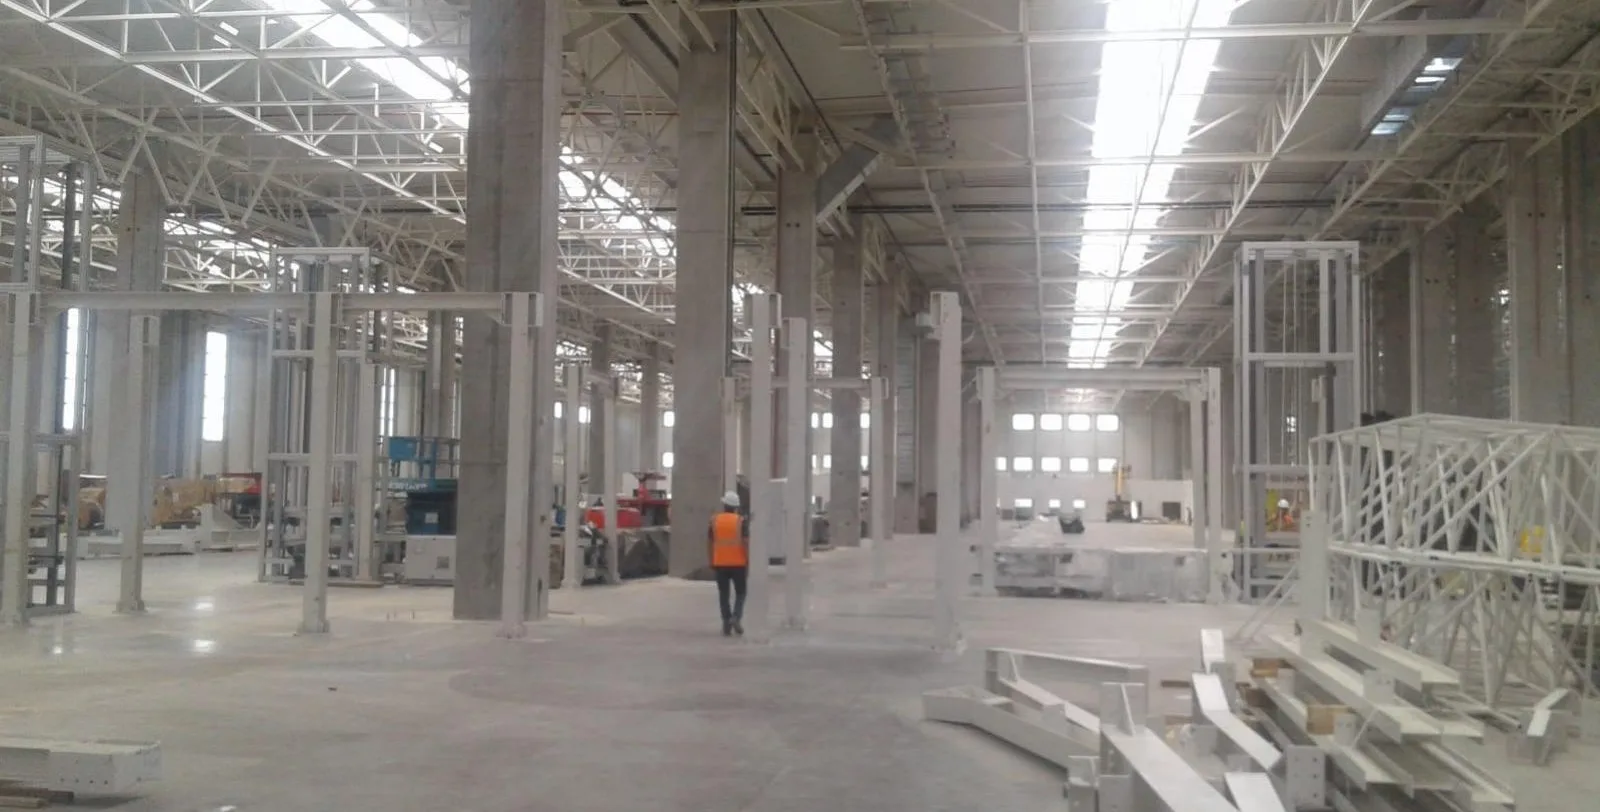
Five service items converge in one field; the following are examples of the part types to which these items are applied.
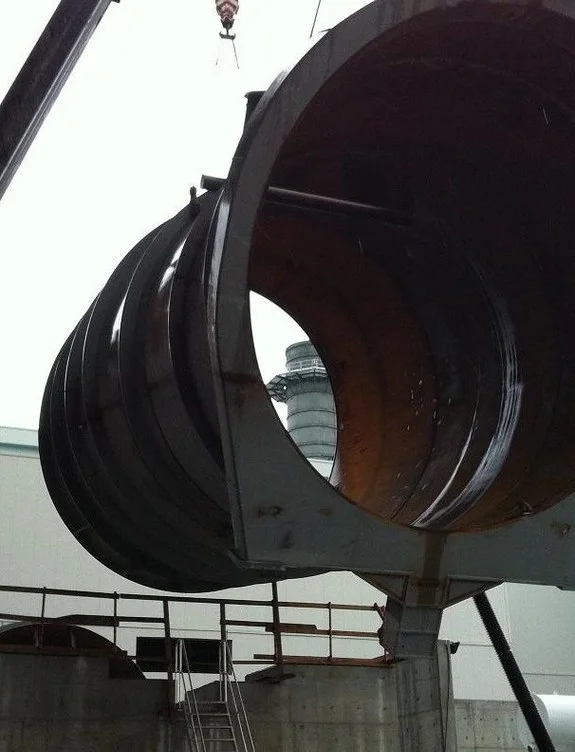
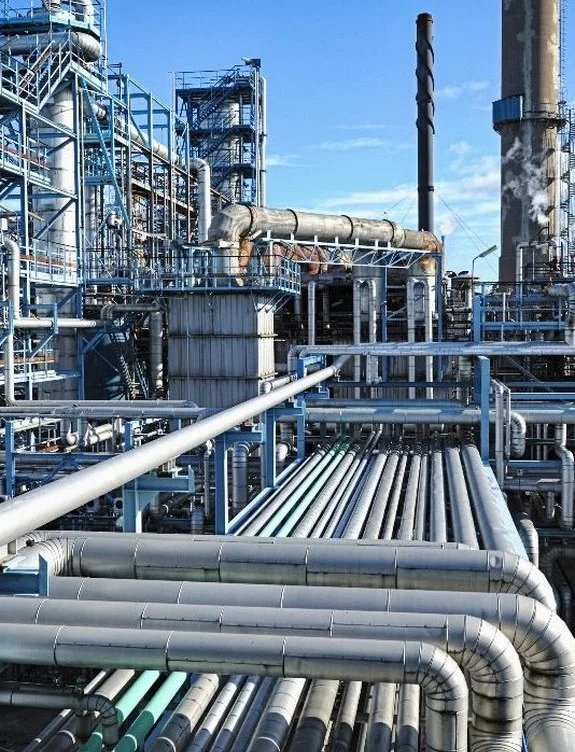
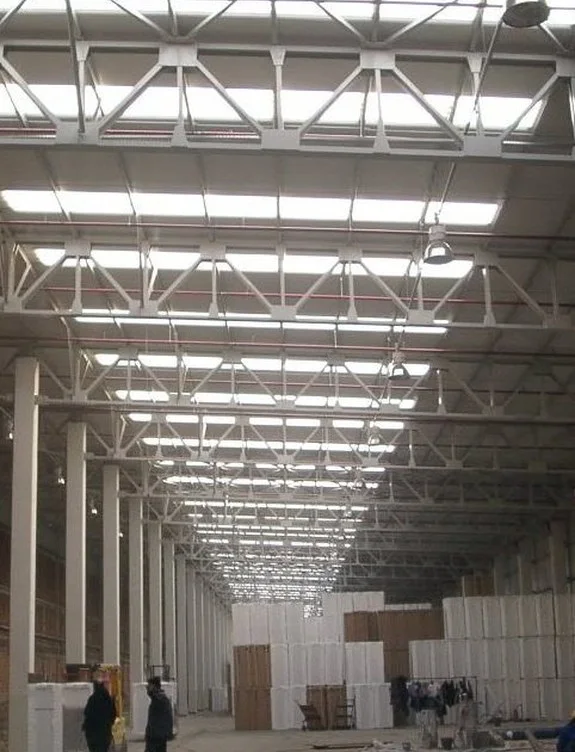
The visuals are taken from the company's own project archive. The applications were carried out in previous years in the facility and application infrastructure where BER-GRİT operates today; project-specific technical details are subject to customer approval.
Let's determine the appropriate service together
When the part list and specification are submitted, the appropriate route, quality scope, and deadline are evaluated by our technical team.
- Specification and drawing file can be attached
- Unknown technical fields can be left blank
- A reference number will be provided after submission