Skip to content
BER-GRİT

Machine park

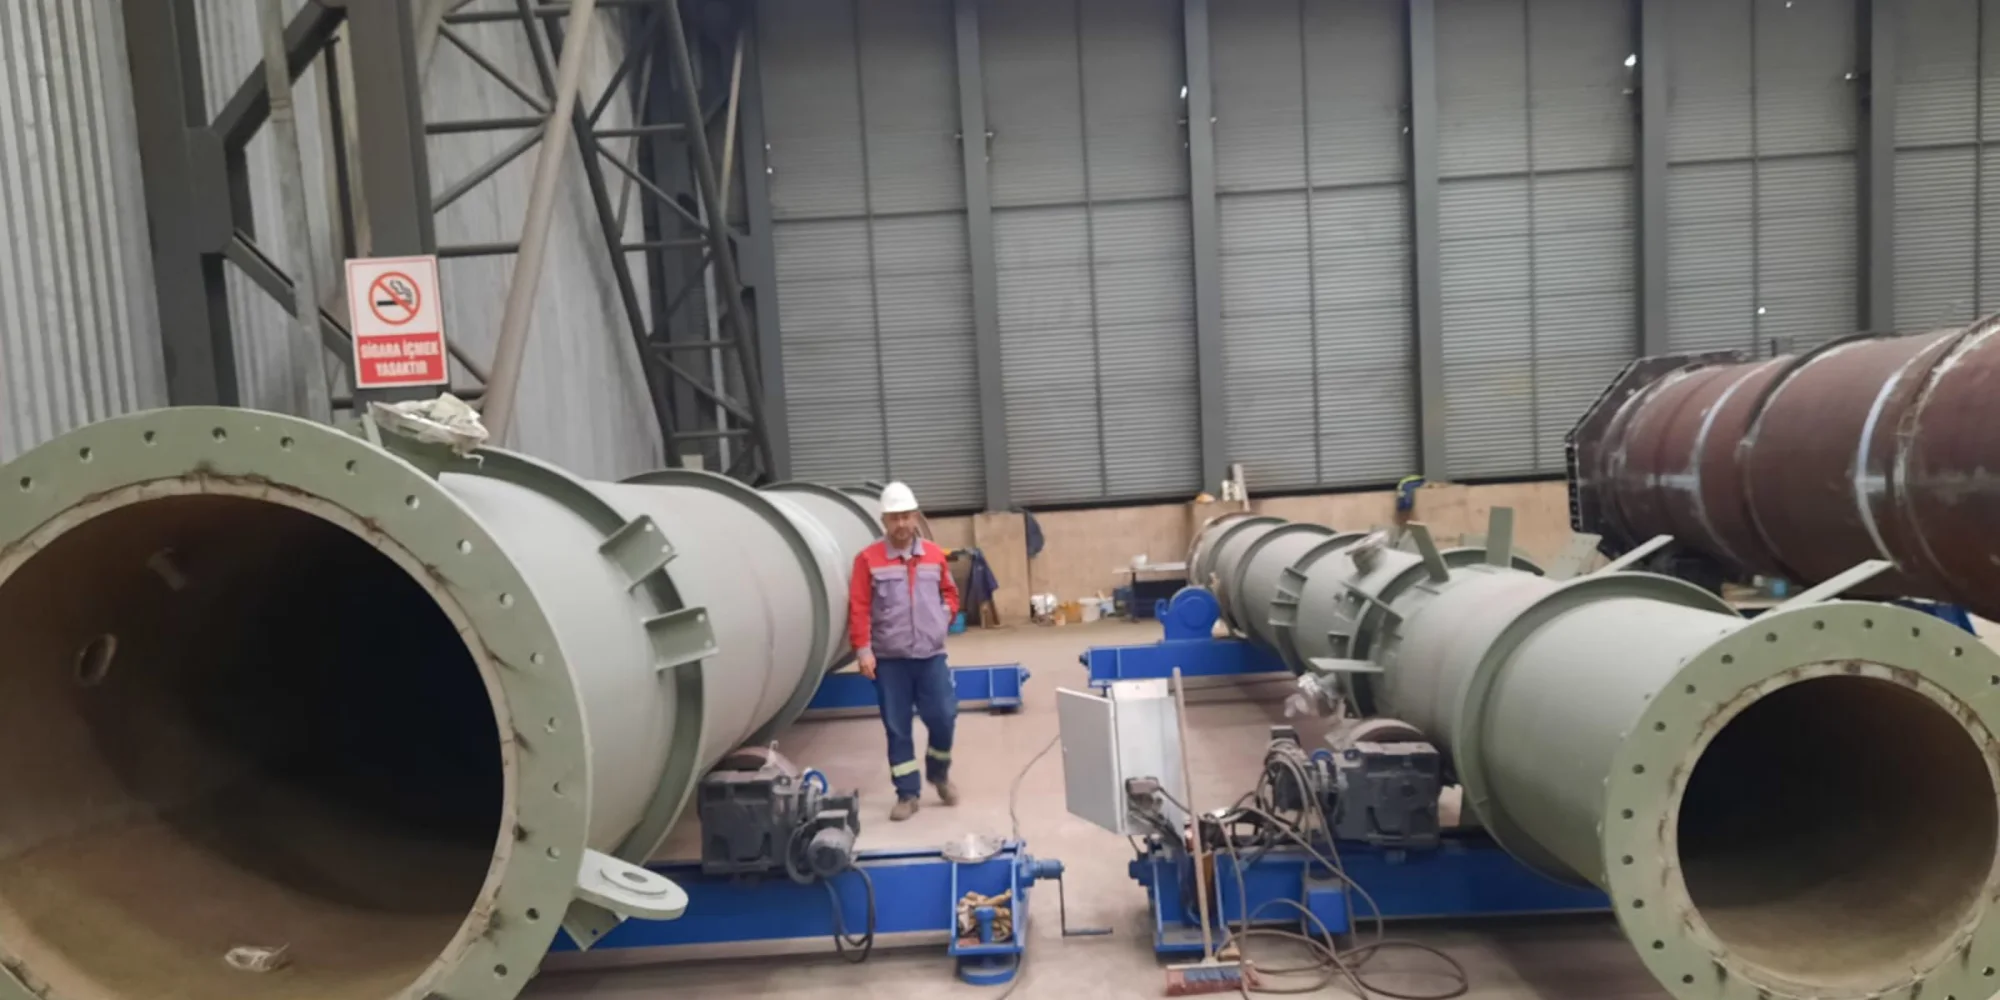
Surface preparation and coating units are arranged under one roof, on a unidirectional flow. The part is not divided according to line constraints; it is taken to the unit suitable for its geometry.

Units and their specifications

The size and geometry of the part, and the surface quality required by the specification determine which unit will be used. The selection is clarified together during the quotation phase.

1. ünite: OMSG LAUCO 150 NP

Automatic turbine blasting line

Continuous tunnel type roller conveyor process for serial steel profiles, sheets, pipes, and repetitive sections. Repeatable surface quality and high throughput speed.

Machine ID

Manufacturer
OMSG · Italy
Model
OMSG LAUCO 150 NP
Year of manufacture
2016
Process
Continuous tunnel, roller conveyor
Suitable parts
Sheet metal, profile, pipe, beam, and steel construction

Key process advantages

  • Continuous flow
  • Homogeneous surface
  • Controlled speed
  • Mass production

Emphasis: Mass, controlled, and repeatable surface preparation for heavy steel construction, sheet metal, and profiles.
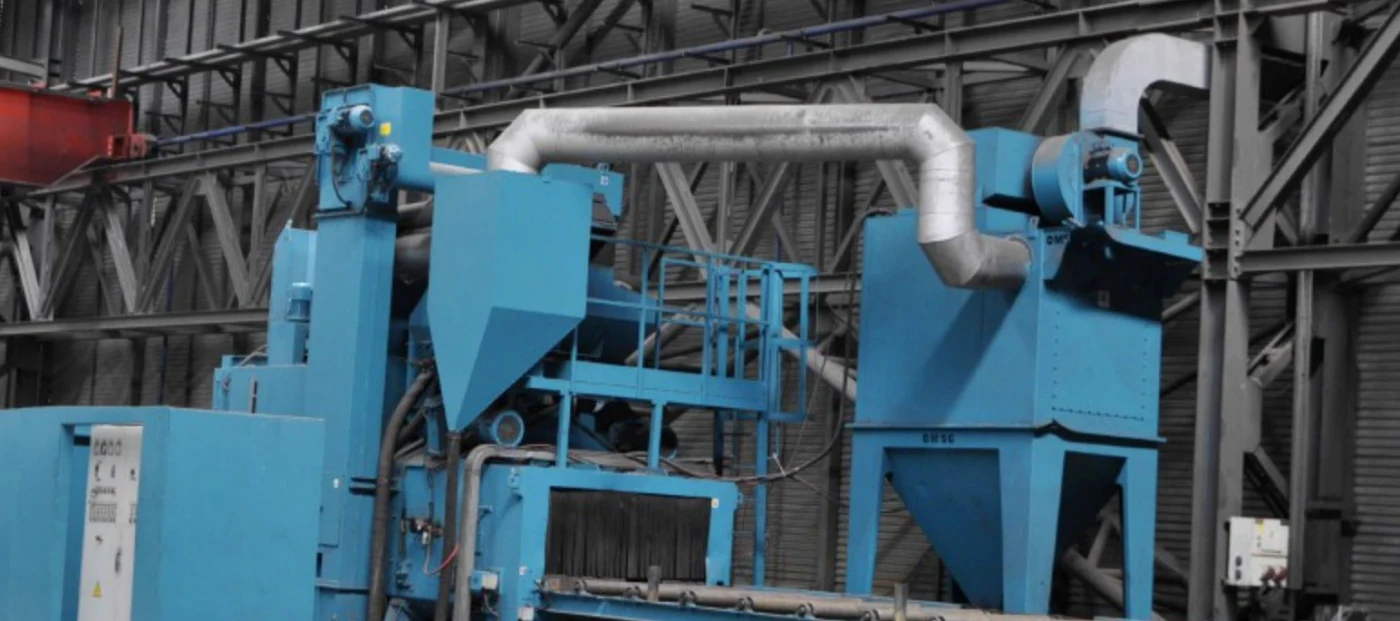
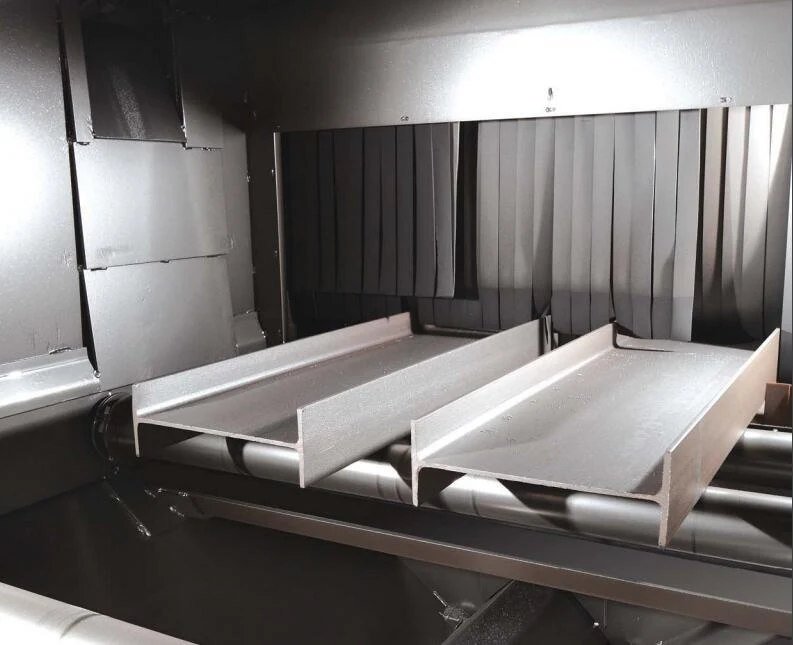
OMSG LAUCO 150 NP automatic turbine blasting line: roller conveyor entry, abrasive recovery cyclone, and filtration unit.

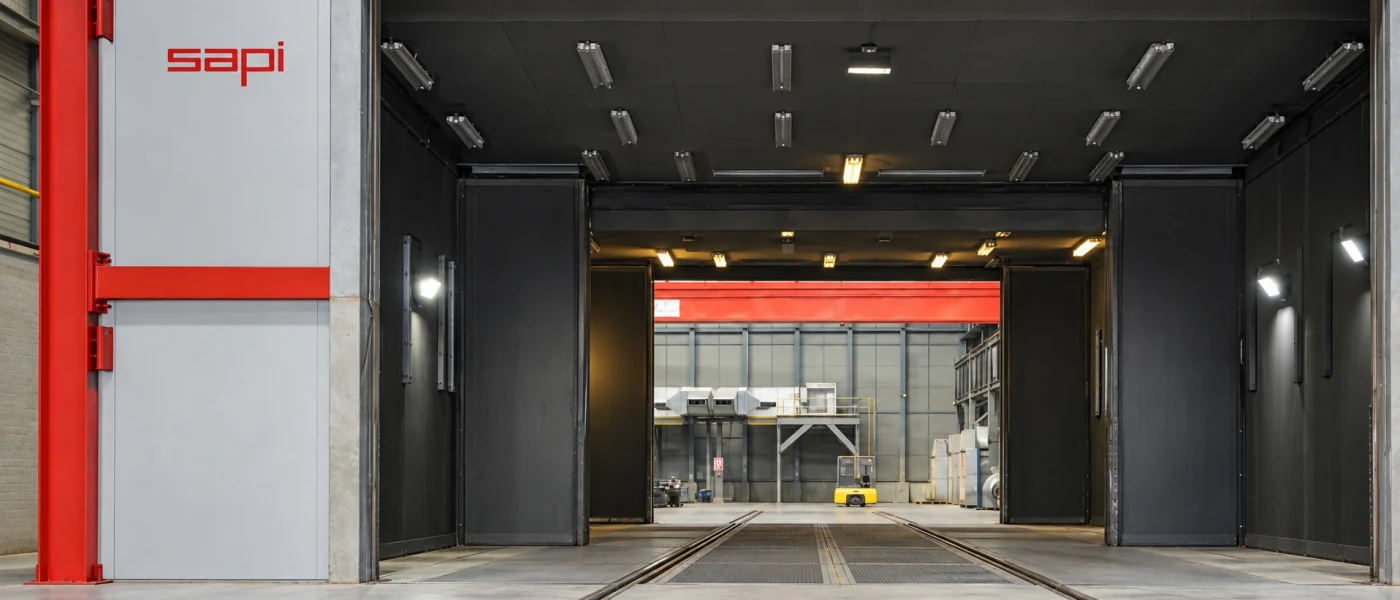
2. ünite: SAPI large volume blasting cabin

Manual operator, double nozzle cabin

For large, heavy, and steel fabrications with different geometries that do not fit in an automatic line. Protruding and box-section parts are processed in a single pass without division.

Machine ID

Manufacturer
SAPI · Almanya
Internal dimensions
8 × 26 × 4,50 m
Nozzle
Çift nozul
Abrasive feed
Automatic recovery and feeding
Suitable parts
Heavy construction, module, equipment body

Key process advantages

  • Indivisible part
  • Double nozzle
  • Flexible geometry
  • Project-based work

Emphasis: Heavy fabrications that do not fit into the automatic line cross-section are processed in one go, without division, according to the line limitation.

Interior volume of the SAPI blasting cabin visible through the open door; part transport rails on the floor and the filtration unit at the end of the cabin.

3. ünite: Paint application unit

Airless application, enclosed hall

After blasting, parts are moved to the paint area within the enclosed hall. Primer, intermediate coat, and topcoat are applied by the airless method; drying and curing continue in the crane area.

Machine ID

Method
Airless spraying
Resin families
Alkyd, epoxy, zinc-rich, polyurethane, intumescent
Corrosivity scope
C3 · C4 · C5
Controls
Climate, WFT, intercoat and total DFT
Drying area
5.000 m² vinçli alan

Key process advantages

  • Indoor area
  • Floor-based control
  • Climate record
  • Drying area with crane

Emphasis: The blasted surface is taken to the painting process without delay; each coat is recorded with its own measurement.

Steel carriers with completed paintwork inside the enclosed hall.

Ongoing investment

Automatic tunnel blasting line

An investment in a new automatic tunnel blasting line with a working opening of 3500 × 1500 mm is ongoing. When the line is commissioned, the capacity and throughput speed for serial production will increase.

The following values are the design specifications of the line. The commissioning schedule and current status will be shared during the quotation phase.

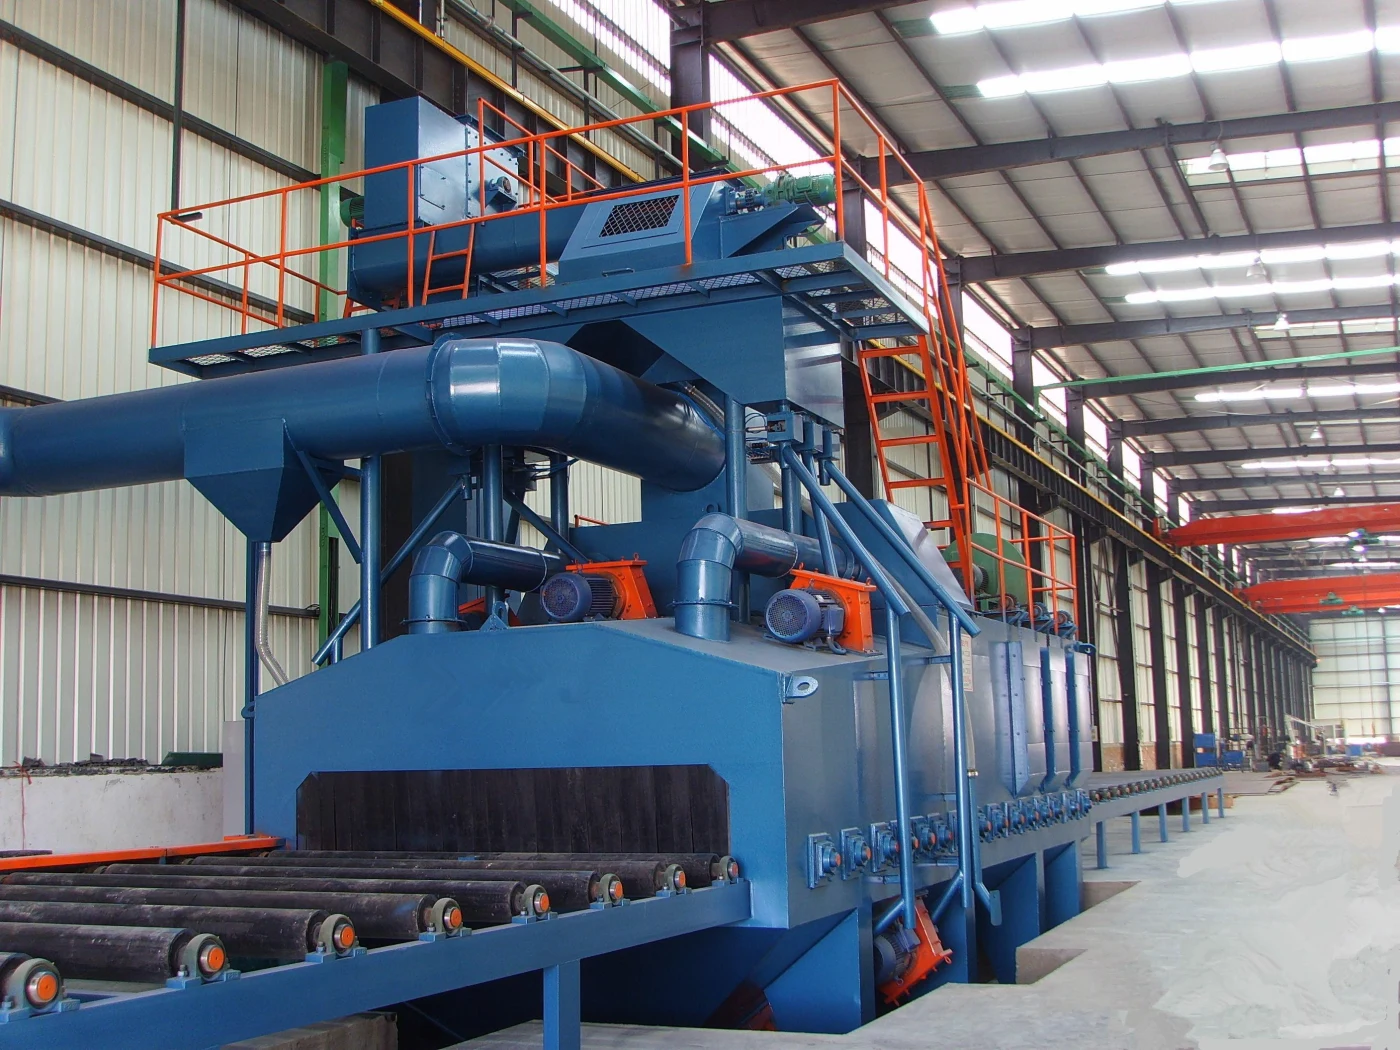
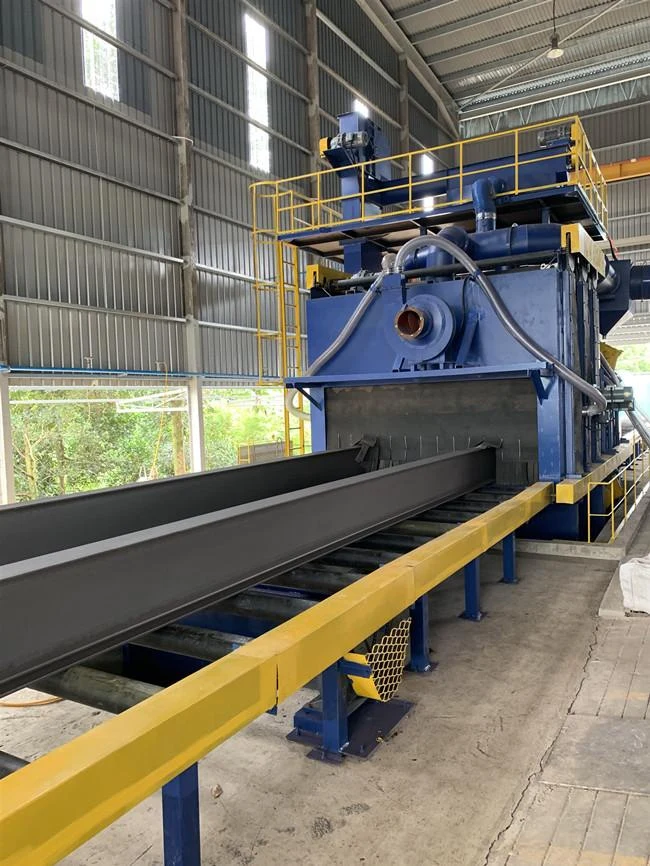
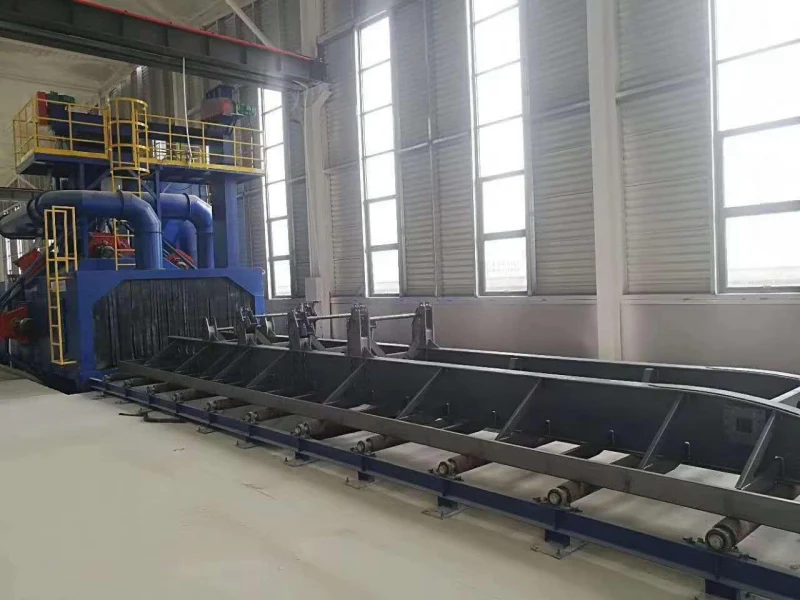
Q6935 type automatic tunnel blasting line: roller conveyor, turbine bodies, abrasive recovery cyclone, and upper service platform.
Supplier reference photo of a line of the same type. It will be replaced with its own photo when the line in the facility is commissioned.
Design specification Q6935
Machine type
Q6935 roller conveyor shot blasting machine
Working opening
3500 × 1500 mm
Maximum workpiece
13000 × 3200 × 1200 mm
Maximum part weight
5 tons
Processing speed
0.5 - 1.0 m/min
Conveyor speed
0.1 - 4 m/min, frequency controlled
Roller conveyor
16 m at input and output
Surface quality
Sa 2½
Surface roughness
40 - 85 µm
Turbines
12 pcs × 11 kW
Shot blasting capacity
Approximately 180 kg/min per turbine
Control system
Siemens PLC and 7-inch HMI
Installed power
234 kW

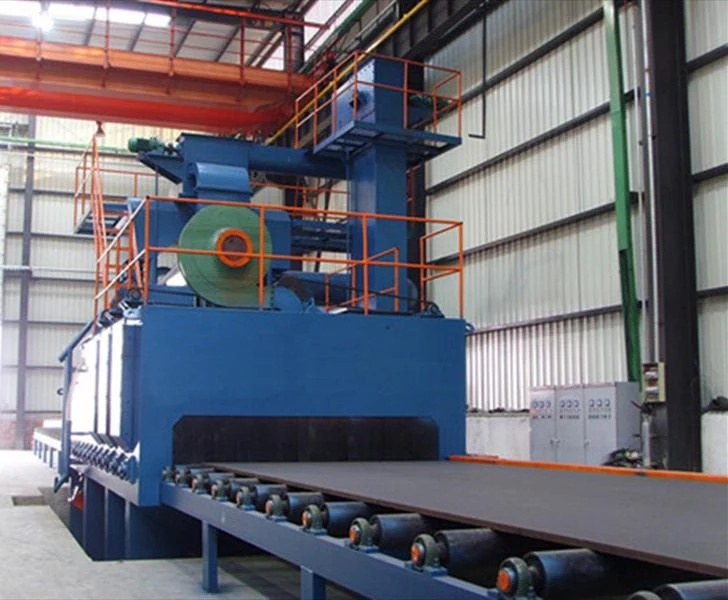
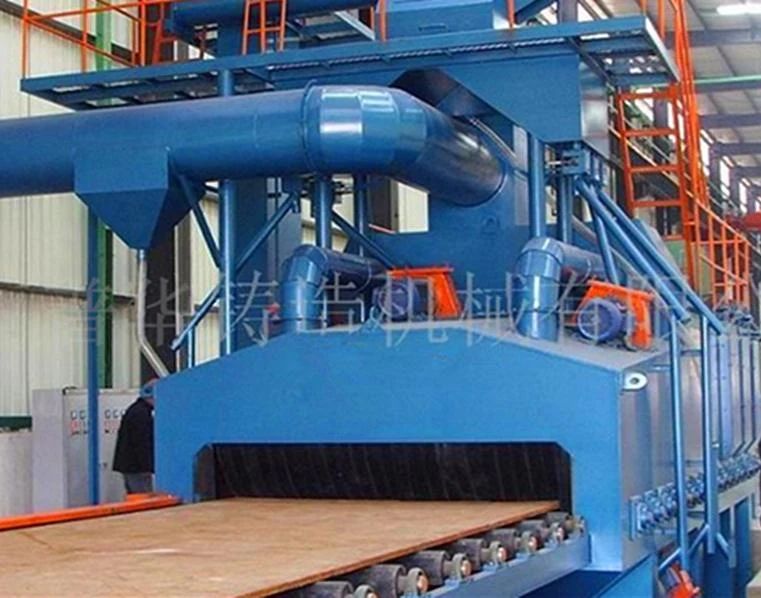
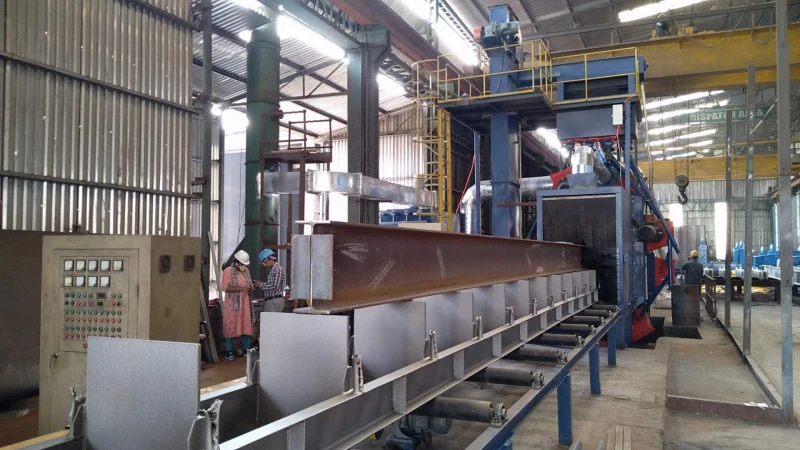
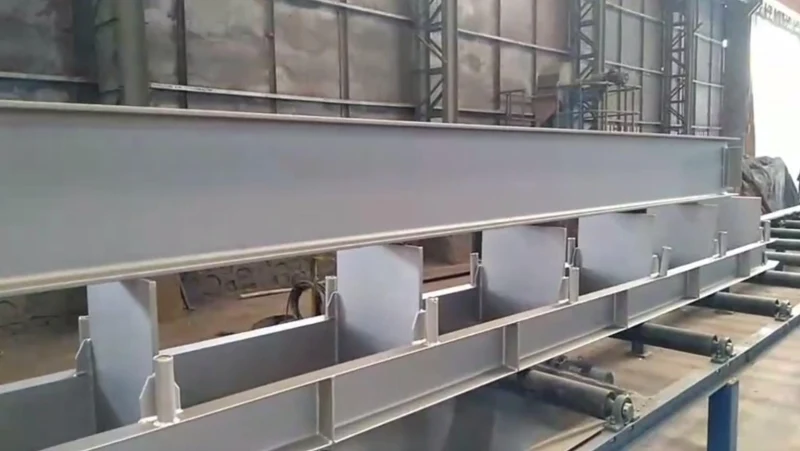
Q6935 tunnel line: supplier references

Examples of the same type of line already commissioned. These images will be replaced with actual photos once the line in our facility starts operating.

The units are on the same flow

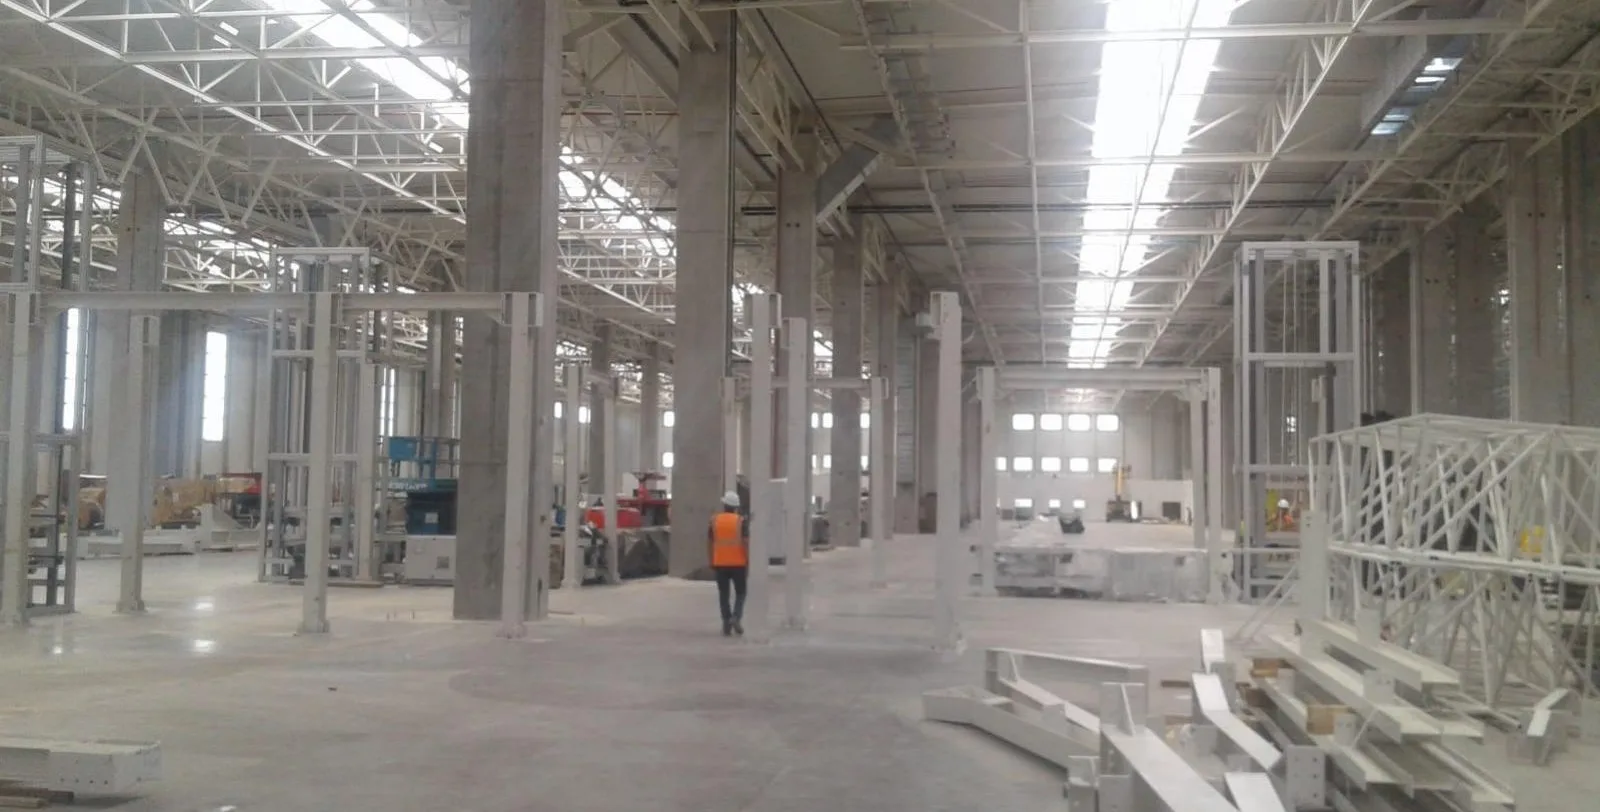
182 meter hall, allowing these units to be arranged in a single direction. Material moves from entry to exit, with no return.

Plant and site layout
Total operation area
10.000m² Total operation area
Enclosed production area
5.000m² Enclosed production area
Weighbridge
2 Weighbridge

Frequently asked questions

The most frequently asked questions during the quotation phase. If you cannot find what you are looking for, you can write directly.

Serial profiles, sheets, pipes, and repeating sections are processed on the OMSG LAUCO 150 NP automatic turbine shot blasting line. Heavy manufactured items that do not fit in the automatic line, have protrusions, or are box sections are processed in the 8 × 26 × 4.50 m SAPI cabin. The decision is made at the quotation stage based on the part's size and geometry.

The OMSG LAUCO 150 NP line is a 2016 production model and has been operating on the same line since that date. It operates with a continuous tunnel-type roller conveyor process.

The SAPI blasting cabin has internal dimensions of 8 meters width, 26 meters length, and 4.50 meters height. As long as the part fits within these dimensions, it is not divided due to line constraints.

An automatic tunnel-type shot blasting line with a working opening of 3500 × 1500 mm is under investment. Once the line is commissioned, capacity and throughput speed for serial jobs will increase. The current status will be shared at the quotation stage.

After blasting, parts are moved to the painting application area within the closed hall. Primer, intermediate coat, and topcoat are applied using the Airless method; the crane-equipped area is used for drying and curing.

Let's determine together which unit is suitable for your part

When part size, weight, and specification are communicated, the suitable unit, terms, and quality scope are evaluated by our technical team.

Example: 40 tons of steel construction, Sa 2½ blasting, zinc epoxy primer and polyurethane topcoat, total 240 µm.

  • Specification and drawing file can be attached
  • Unknown technical fields can be left blank
  • A reference number will be provided after submission